Build the operation
Manage four engineers across digitalization, process, and manufacturing test. Own goals, performance reviews, development plans, and work allocation.
Turning a PCB-stator motor architecture into a staffed, qualified manufacturing operation—and questioning which operations needed to exist at all.
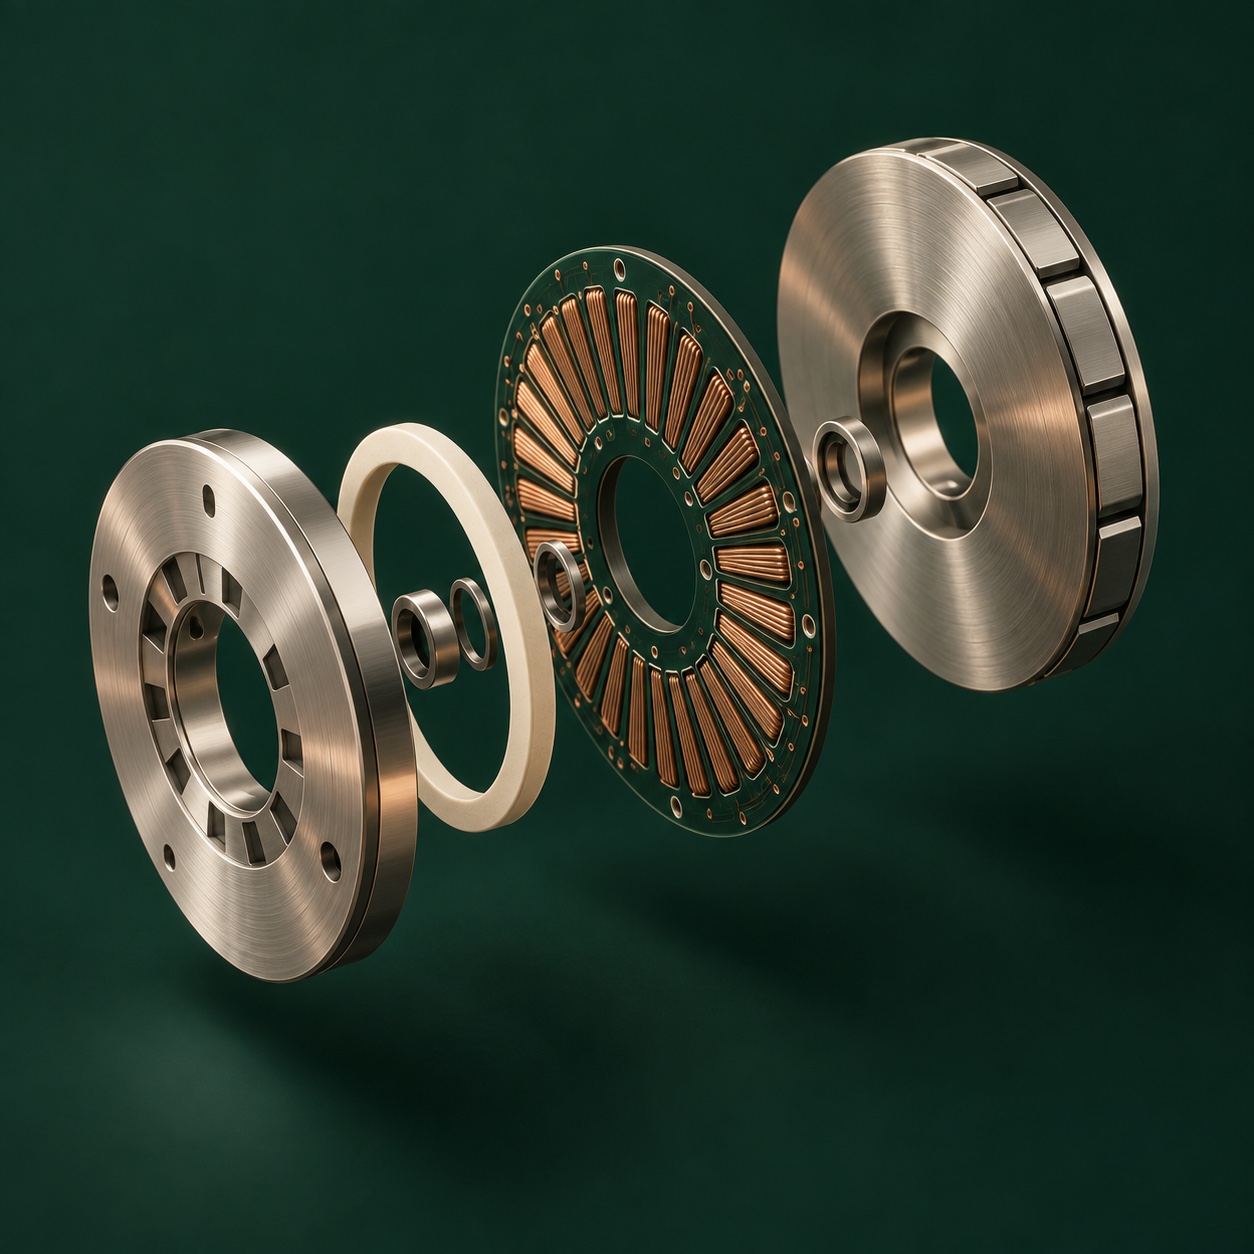
Infinitum’s air-core electric motors use a PCB stator. Manufacturing that architecture required developing and proving assembly methods instead of simply adopting an established motor-production line.
I lead advanced manufacturing engineering, managing four engineers across digitalization, process, and manufacturing test and coordinating NPI readiness with engineering, quality, supply, and manufacturing partners. The work was to turn bench-proven methods into an operation with defined routing, fixtures, process windows, operator instructions, and inspectable results.
Explore Infinitum’s motor technology ↗The tradeoffKeeping an operation can feel safer than making the case to remove it. It also preserves its time, material, and handling burden.
My responseRemoved an adhesive operation, thermal dispense under the inductors, and an in-process electrical test after the data supported their removal.
What supported the decisionEliminating those three steps reduced assembly time by approximately 12%.
The tradeoffA method that works at the bench still needs to hold across operators and production conditions.
My responseDefined assembly sequences, fixtures and tooling, and process windows for critical steps. Qualified 12 processes.
What supported the decisionDocumented methods and process limits made the work repeatable and inspectable by the production team.
The tradeoffA control chart makes variation visible; the line still needs a defined response when a signal appears.
My responsePut critical characteristics under SPC, with control charts, capability studies, and reaction plans.
What supported the decisionMeasurements were connected to part, station, and recipe through the manufacturing data system, supporting traceability and investigation.
Manage four engineers across digitalization, process, and manufacturing test. Own goals, performance reviews, development plans, and work allocation.
Coordinated the contract-manufacturing and supplier partners the ramp depended on.
Used structured root-cause work to isolate contributing variables and carry corrective actions back into the process.
I co-led two product-line launches, owning process flow, station sequencing, test strategy, and data infrastructure; equipment scope was shared with a peer manager. I also led NPI transfers from the US prototype hub to production in Mexico, with risk planning and readiness gates. I joined Infinitum as Advanced Manufacturing Engineering Manager in October 2023 and became Senior Manager in April 2026.
Three operations were eliminated, reducing assembly time by approximately 12%. Twelve processes were qualified. Alongside that process work, I built the business case for an in-house MES and led its delivery across production plants in the US and Mexico.
The assembly-time improvement came from removing those three operations. Total line throughput also depends on the bottleneck, staffing, and yield—a different question from time removed from the assembly route.